Introduction
A large OPzV or OPzS order may contain:
- 24 cells
- 55 cells
- 108 cells
- 110 cells
- Several complete battery banks
with individual capacities ranging from a few hundred Ah to 3000Ah or more.
Once these batteries are shipped internationally, correcting a factory problem becomes much more expensive.
A missing connector discovered at the factory is a small issue.
The same missing connector discovered during commissioning at a remote substation can delay an entire project.
The same principle applies to:
- Wrong cell quantity
- Incorrect polarity arrangement
- Abnormal OCV
- Damaged terminals
- Incorrect dimensions
- Capacity disagreement
- Missing rack hardware
- Incorrect labels
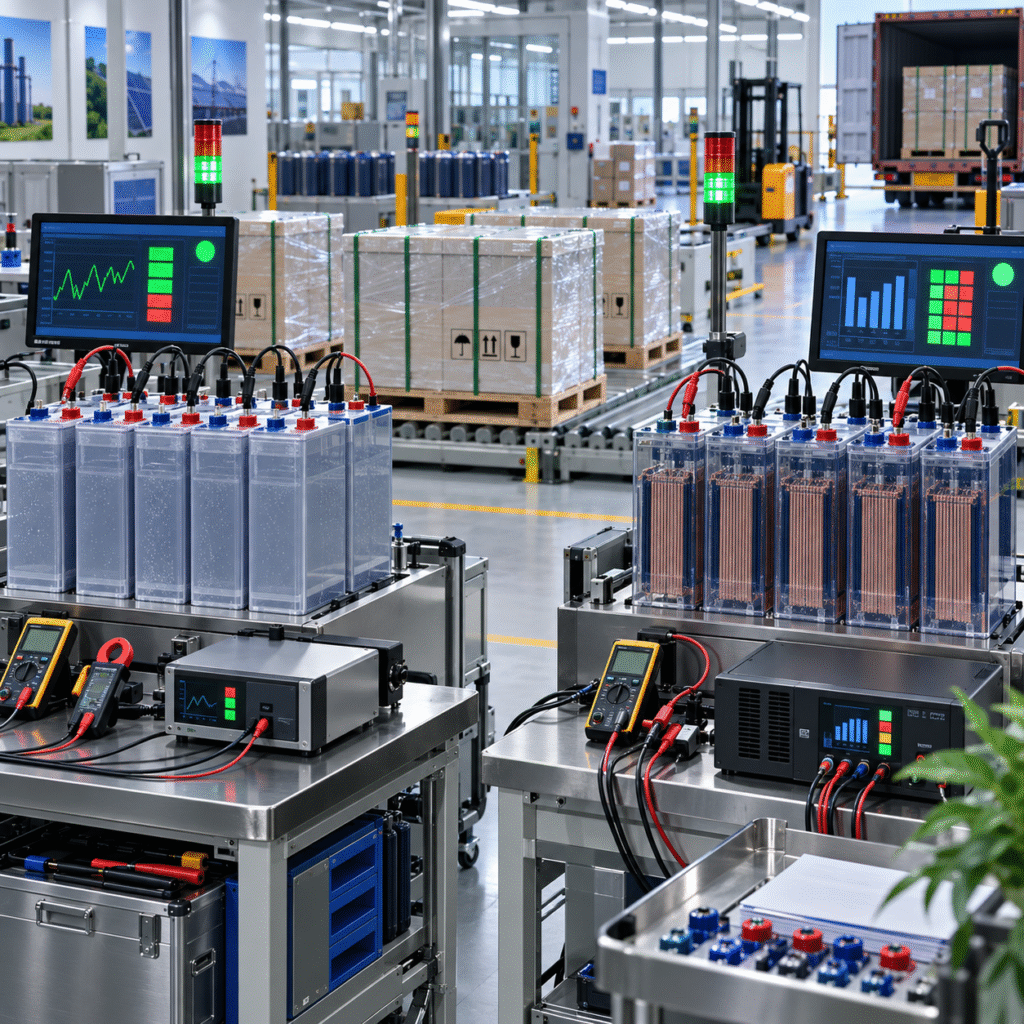
This is why large B2B battery projects should define a Factory Acceptance Test, or FAT, before shipment.
WUXI HUIZHONG POWER states that its cells are verified and tested before shipment, but project buyers should still define the specific inspection and documentation they require for their own contract.
Factory QC and FAT Are Not Exactly the Same Thing
Routine factory quality control belongs to the manufacturer’s normal production process.
It may include:
- Incoming material inspection
- Plate-production control
- Assembly checks
- Charging
- Voltage testing
- Final inspection
A project FAT is different.
The FAT establishes:
What evidence does this specific customer require before approving this specific shipment?
For example, a utility project may require:
- Individual cell OCV
- Individual resistance
- Capacity-test records
- Serial-number list
- Dimensional inspection
while a distributor buying standard stock may require a simpler inspection.
The FAT should therefore be agreed before production is completed.
Step 1: Confirm the Approved Battery Specification
Before testing begins, compare the finished batteries with the approved technical data.
Check:
- Battery type
- Nominal voltage
- Rated capacity
- Capacity rating basis
- Model number
- Terminal type
- Dimensions
- Weight
- Applicable standard
For OPzV stationary VRLA batteries used in float standby applications, IEC 60896-21 specifies test methods and IEC 60896-22 provides the corresponding requirements framework.
For vented OPzS stationary batteries, IEC 60896-11 covers general requirements and test methods.
The tender should clearly identify which standards actually apply to the project.
Step 2: Verify Capacity Rating Conditions
Do not verify only:
2V 1000Ah
A proper check should include:
1000Ah at what discharge rate?
For example:
- C10
- 8-hour rate
- C5
Then check:
- End-of-discharge voltage
- Reference temperature
One current OPzV product range, for example, lists European capacity using C10 to 1.80V/cell at 20°C, while its U.S. rating uses an 8-hour discharge to 1.75V/cell at 77°F.
This illustrates why Ah alone is not a complete acceptance criterion.
Step 3: Visual Inspection of Every Cell
Every battery should be checked for:
- Cracked container
- Case deformation
- Damaged cover
- Terminal damage
- Incorrect polarity marking
- Dirty surface
- Leakage
- Missing labels
For OPzV, pay particular attention to:
- Case swelling
- Valve area
- Terminal-to-cover seal
For OPzS, also inspect:
- Vent caps
- Transparent container
- Electrolyte condition if supplied filled
Visual inspection is simple but can prevent many later disputes.
Step 4: Check Model and Serial Numbers
For a large project, prepare a serial-number register.
Example:
| Position | Model | Serial Number | Production Date |
|---|---|---|---|
| Cell 001 | |||
| Cell 002 | |||
| Cell 003 |
This creates traceability between:
- Factory production
- Shipment
- Installation
- Warranty
If a future fault occurs in Cell 37, both supplier and customer can identify exactly which product is involved.
Step 5: Measure Individual Open-Circuit Voltage
OCV should be measured using a calibrated meter under consistent conditions.
The purpose is not simply to check whether a cell shows “around 2V.”
The more useful information is the distribution.
Example:
- Cell 001: 2.13V
- Cell 002: 2.13V
- Cell 003: 2.12V
- Cell 004: 2.13V
- Cell 005: 2.05V
Cell 005 is an obvious outlier that should be investigated before shipment.
Do not average the whole bank and ignore individual deviations.
Step 6: Record Internal Resistance or Conductance
For OPzV projects, an individual resistance or conductance report is valuable because it establishes a new-battery baseline.
This baseline can later be compared with:
- Year 1
- Year 3
- Year 5
- Year 8
maintenance readings.
IEEE 1188-2025 is the current IEEE recommended practice covering maintenance, testing and replacement of stationary VRLA batteries.
Although FAT requirements are contractual, collecting baseline electrical data before shipment makes future condition monitoring much more useful.
Do Not Use Resistance Alone as a Capacity Test
This distinction should be written into the FAT.
Internal resistance can reveal:
- Outliers
- Connection problems
- Possible weak cells
but it does not directly prove:
1000Ah capacity.
If capacity verification is contractually required, a controlled discharge test should be defined separately.
Step 7: Decide Whether Capacity Testing Is 100% or Sample-Based
Testing every large OPzV or OPzS cell individually to full rated capacity can be:
- Time-consuming
- Expensive
- Operationally unnecessary
depending on the project.
A tender may instead specify:
- Full-bank test
- Sample capacity test
- Production-batch sample
- Witnessed test on selected cells
There is no universal rule that every shipment must use the same FAT sampling plan.
The customer and manufacturer should agree before production.
Capacity-Test Conditions Must Be Written Clearly
The FAT should state:
- Test battery model
- Test current
- Test duration
- Final voltage
- Battery temperature
- Required result
For example, do not simply write:
“Battery must reach 1000Ah.”
Write the actual rating basis.
Otherwise, a capacity dispute can occur even when both parties are technically correct under different test conditions.
Step 8: Confirm the Battery Is Fully Charged Before Capacity Testing
A new battery cannot reasonably be judged against full rated capacity if it has not received the proper commissioning charge.
For OPzV, charging condition before testing matters significantly.
IEEE 1188 covers formal testing methodology for stationary VRLA batteries, while the battery manufacturer’s charging instructions should determine how the new battery is prepared for the test.
Do not perform a capacity test immediately after long storage without first establishing the correct SOC.
Step 9: Monitor Individual Cell Voltage During a String Test
If a complete battery string is discharged, record individual cell voltages.
This allows the test to answer two questions:
- Does the complete bank deliver sufficient capacity?
- Is one cell substantially weaker than the others?
A total string voltage alone can hide one deteriorating cell.
Step 10: Confirm Dimensions
Dimensional inspection becomes particularly important for replacement projects.
Check:
- Length
- Width
- Container height
- Total height
- Terminal spacing
A technically correct 2V 1000Ah battery that cannot fit the customer’s existing rack can still cause project failure.
For replacement tenders, compare the final manufactured dimension with the approved drawing.
Step 11: Check Battery Weight
Weight is useful as a production-consistency check.
The FAT can compare actual weight with the approved tolerance.
However:
Weight should not be used as the only measure of battery quality.
A heavier battery is not automatically better.
Weight should be evaluated together with:
- Capacity
- Discharge data
- Construction
- Dimensions
Step 12: OPzS Electrolyte Inspection
If OPzS batteries are supplied filled and charged, the FAT may include:
- Electrolyte level
- Specific gravity
- Electrolyte temperature
IEC 60896-11 applies to vented stationary batteries such as OPzS.
The required SG must match the specific manufacturer’s product.
Do not adopt a generic acid-density value from another brand.
Step 13: Dry-Charged OPzS Requires a Different FAT
If batteries are shipped dry charged, the FAT cannot use the same electrolyte checks as a filled battery.
Instead verify:
- Dry-charge condition
- Sealing
- Supplied electrolyte specification, if included
- Filling instructions
- Commissioning manual
The shipment documents should make it completely clear who is responsible for:
- Electrolyte supply
- Filling
- Initial charging
at destination.
Step 14: Terminal and Connector Inspection
Check:
- Terminal size
- Thread
- Polarity
- Intercell connector size
- Insulation covers
- Fasteners
For a 110V or 220V DC system, a missing set of copper connectors can prevent commissioning of the entire bank.
Count accessories before packing.
Step 15: Battery Rack FAT
If the order includes battery racks, inspect them as part of the same project.
Check:
- Rack dimensions
- Number of tiers
- Number of cells per row
- Steel thickness according to approved drawing
- Surface coating
- Bolts
- Bracing
- Labels
The battery and rack should be considered one installation system.
Step 16: Trial Assembly Can Be Valuable
For a customized rack, consider assembling:
- Several cells
- Intercell connectors
- Rack section
before shipment.
This can identify:
- Incorrect spacing
- Connector mismatch
- Terminal-clearance problems
before equipment travels thousands of kilometers.
Step 17: Verify Charger Compatibility Information
The battery FAT does not necessarily test the customer’s charger, but the supplier should provide:
- Float voltage
- Boost voltage
- Recommended current
- Temperature compensation
- End-of-discharge information
This allows the EPC contractor to configure the rectifier correctly.
Step 18: Check Labels and Nameplates
Verify that the nameplate clearly identifies:
- Manufacturer
- Model
- Nominal voltage
- Capacity
- Production information
If the project requires:
- Customer logo
- Project number
- Cell position label
check these before packing.
Step 19: Review Certificates and Documentation
Depending on the contract, the shipment file may include:
- Data sheet
- Installation manual
- Test report
- Certificate of conformity
- IEC documentation
- ISO certificate
- Packing list
- Commercial documents
Do not wait until customs clearance or tender handover to discover that a required document was not prepared.
Step 20: Photograph the Finished Batteries
Take clear photographs of:
- Complete battery
- Labels
- Terminals
- Pallets
- Wooden cases
- Rack components
For custom projects, share these with the customer before shipment.
This provides a final visual confirmation.
Step 21: Inspect Packing
Large 2V cells are heavy.
Packing should prevent:
- Tipping
- Terminal impact
- Cell movement
- Case abrasion
The battery may pass every electrical test but still be damaged during shipping if packaging is inadequate.
Recommended FAT Report Structure
Section A — Project Information
- Customer
- Project
- Purchase order
- Battery model
- Quantity
Section B — Physical Inspection
- Appearance
- Dimensions
- Weight
- Terminal condition
Section C — Electrical Data
- OCV
- Internal resistance/conductance
- Capacity test if applicable
Section D — OPzS Data
- SG
- Electrolyte level
- Temperature
Section E — Accessories
- Connectors
- Covers
- Rack
- Hardware
Section F — Documents
- Manuals
- Certificates
- Test records
Section G — Final Approval
- Manufacturer
- Customer/third-party inspector
- Date
Remote FAT for International Buyers
The customer does not always need to send an engineer to China.
A practical remote FAT can include:
- Live video inspection
- Serial-number verification
- Random OCV testing
- Random resistance testing
- Capacity-test video
- Digital FAT report
This can be useful for distributors and EPC contractors trying to control travel cost.
For high-value utility projects, a third-party inspection company may also witness the FAT.
Factory FAT Is Not the Same as Site Acceptance Testing
This distinction is important.
FAT
Performed before shipment.
Confirms:
- Product
- Specification
- Manufacturing condition
SAT / Site Acceptance
Performed after installation.
Confirms:
- Installation
- Charger settings
- Connections
- String voltage
- Site performance
A battery can pass FAT and still perform poorly if it is incorrectly installed or charged at site.
Frequently Asked Questions
Should every OPzV cell receive a capacity test before shipment?
Not necessarily. The test scope should be defined contractually according to project requirements.
Should every cell have OCV measured?
For large project orders, recording individual cell voltage is a useful and relatively simple QC/FAT step.
Can internal resistance prove battery capacity?
No. It is useful for baseline and fault screening but does not replace a controlled capacity test.
Which standard applies to OPzV?
IEC 60896-21/22 applies to stationary valve-regulated lead-acid batteries for float standby applications.
Which standard applies to OPzS?
IEC 60896-11 applies to vented stationary lead-acid batteries.
Should FAT requirements be agreed before production?
Yes. This prevents disagreements about test methods and acceptance criteria after the batteries are completed.
Conclusion
For a large OPzV or OPzS project, FAT should answer one simple question:
Is the product leaving the factory the same product that the customer approved and ordered?
A strong FAT can include:
visual inspection + dimensions + weight + OCV + resistance baseline + capacity verification + electrolyte checks + accessories + rack + documents + packing.
For distributors and EPC contractors, defining these requirements before production can substantially reduce technical and commercial disputes after shipment.