Introduction
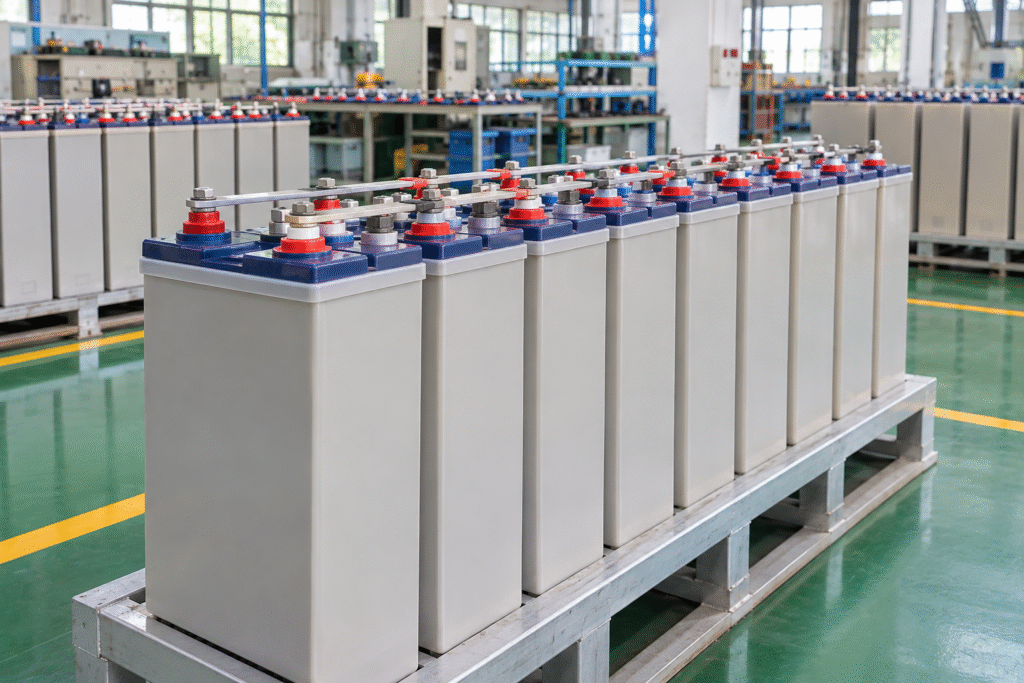
An industrial nickel-cadmium battery manufacturer completes production and provides a factory test report showing that the batteries meet the agreed specifications. The shipment is delivered to an overseas power plant or electrical substation, where the EPC contractor installs the battery bank and performs a site acceptance test.
Unexpectedly, the battery fails to achieve the required discharge duration. The contractor believes the manufacturer supplied defective batteries. The manufacturer refers to its successful factory test results. Meanwhile, the end user demands a solution before approving project handover.
This situation can create a difficult dispute involving battery quality, installation conditions, testing methods, warranty obligations, and project scheduling. However, a successful factory test and an unsuccessful site test do not automatically identify which party is responsible. The first step is to establish whether the tests were comparable and what changed between manufacturing and site commissioning. This article explains how international battery importers, EPC contractors, and industrial battery manufacturers can investigate these disagreements systematically.
1. Factory Acceptance Testing and Site Acceptance Testing Have Different Purposes
Factory acceptance testing (FAT) and site acceptance testing (SAT) are important stages in industrial battery supply projects, but they do not necessarily evaluate identical conditions. Factory testing is conducted before delivery and may include product inspections, electrical measurements, performance testing, and review of required manufacturing records. Site acceptance testing is performed after installation and is generally intended to verify that the supplied equipment meets the approved project requirements under the relevant commissioning conditions.
Factory Acceptance Testing
A factory test may be conducted under controlled temperature, charging, and discharge conditions. The test can provide evidence that the battery cells meet specified performance requirements at the time of testing. However, the extent of testing depends on the agreed procedure. For example, a factory inspection of selected sample cells does not necessarily establish that every delivered cell has undergone an identical full-capacity discharge test. The test report should clearly identify the tested products, conditions, and results.
Site Acceptance Testing
The site test may involve the installed battery bank, intercell connectors, charger, battery cables, and project-specific acceptance requirements. Consequently, site results can be affected by additional factors that were not present during factory testing.
These may include installation quality, storage conditions, charging preparation, equipment settings, and environmental temperature. The contract should define the precise scope and acceptance criteria of both tests.
2. Were the Factory and Site Tests Actually Comparable?
This is often the most important question in a disputed battery project. A battery may have been tested at the factory using one discharge current and final voltage, while the site test uses different conditions. Even small differences in the test procedure can influence the recorded result.
Example: Different Discharge Conditions
Suppose a 200Ah industrial NiCd battery was tested at the factory according to the approved reference capacity procedure. At the site, the contractor performs a discharge using a higher current because the project has a demanding emergency load profile. The result is shorter than expected. This does not automatically mean that the factory report was incorrect.
The battery may meet its specified rated capacity but fail to satisfy a different discharge requirement. The engineering question is whether the originally supplied model was correctly selected for the contractual duty. If the tender required the higher-rate performance and the supplier offered a technically unsuitable product, the issue may be related to product selection or contractual compliance. If the site test differs from the approved requirements, the test procedure itself may need correction.
3. Initial Charging and Commissioning History Can Change the Result
Industrial NiCd batteries require appropriate charging preparation before acceptance testing. The correct procedure depends on the cell design, delivery condition, storage history, and manufacturer’s instructions.
A battery may have passed its factory test, then spent several months in transportation or storage before reaching the installation site. It may subsequently be tested before completing the required commissioning process.
Example: Delayed Power Plant Project
A power plant purchases a new industrial NiCd battery bank. The manufacturer completes factory testing and ships the products. Construction delays prevent the contractor from installing them for several months. Once installation begins, the contractor charges the battery for a short period and immediately performs a discharge test.
The battery does not achieve the required duration. In this situation, the investigation should review the shipment condition, storage conditions, charging preparation, and commissioning procedure. The initial failed result should be documented, but the cause cannot be determined without this information.
4. Could Transportation or Storage Have Affected the Batteries?
International battery shipments may involve multiple handling and storage stages. Products may be transported from the factory to a port, loaded into containers, shipped overseas, cleared through customs, and stored at a project warehouse.
During these stages, the batteries may experience mechanical stress or environmental conditions outside the manufacturer’s recommendations. A successful factory test cannot prove that no damage occurred after the test.
What Evidence Is Useful?
The receiving inspection report, shipment photographs, packaging records, storage temperatures, and installation history can help establish the condition of the batteries after delivery. If cell containers or terminals were damaged during transport, the issue may be unrelated to the original manufacturing quality. However, commercial responsibility for such damage depends on the contract, applicable transport terms, and circumstances. It should not be assigned solely on the basis of the eventual site test failure.
5. Installation Problems Can Produce Apparent Battery Performance Failures
An installed battery bank includes more than individual electrochemical cells. Intercell connections, terminal hardware, DC cables, protective devices, and electrical monitoring equipment can influence the result. For example, a high-resistance connection may cause additional voltage drop under discharge current.
If the discharge test monitors only total voltage at a remote measurement point, this voltage loss may cause the test to stop earlier than expected. The technician might incorrectly conclude that the cells have insufficient capacity.
Recommended Technical Investigation
The project team should examine connection condition, terminal installation, voltage drop, cell configuration, polarity, and test equipment measurement points. Where appropriate, individual cell voltage measurements can help distinguish a cell-related problem from an external connection issue. All inspections and corrective work should follow site electrical safety requirements. For critical DC power systems, the availability of essential control and protection functions must be maintained during troubleshooting.
6. Incorrect Test Equipment Settings Can Create a False Failure
Electronic discharge testers and data acquisition systems must be correctly configured. An incorrect current setting, final-voltage threshold, cell count, or measurement calibration can change the reported result. For example, if the discharge endpoint is set above the approved voltage, the tester may stop before the battery has completed the intended discharge.
Similarly, a current setting above the specified value can shorten the discharge duration. A complete investigation should examine the raw test records rather than relying only on a summary stating that the battery failed.
Important Test Records
The most useful records include discharge current, battery voltage, individual cell voltages where available, temperature, elapsed time, final voltage, and the instrument’s settings. Calibration information may also be required by the project contract. Test equipment data can help determine whether the reported failure reflects actual battery behavior or an incorrect measurement procedure.
7. A Factory Test Report Must Be Reviewed Carefully
The presence of a factory test report is useful but does not eliminate the need for technical evaluation. Some reports contain only routine inspection results. Others include detailed electrical measurements and discharge performance data. The buyer should identify exactly what the report demonstrates.
Questions to Ask
Does the report identify the correct battery model and production batch? Were all cells tested, or were samples selected? What charging procedure was used? What were the discharge current, temperature, final voltage, and acceptance criteria? Was the test performed before shipment, and were the results witnessed by an authorized third party if the contract required it?
These details matter because a report can be authentic yet insufficient to demonstrate compliance with a particular project requirement. IEC 60623:2026 provides a relevant framework for testing industrial vented NiCd cells and battery systems, but project-specific FAT and SAT requirements must still be agreed and documented. IEC
8. Who Is Responsible When the Site Test Fails?
There is no universal answer. Responsibility depends on the verified technical cause and the contractual obligations of each party. A manufacturing defect may point toward the battery supplier. Incorrect installation or commissioning may point toward the responsible contractor. Transportation damage, unsuitable storage, or an incorrect system design can involve other parties.
Illustrative Responsibility Matrix
| Confirmed Problem | Party or Responsibility to Investigate |
|---|---|
| Battery fails agreed product requirements despite valid testing | Manufacturer or contractual supplier |
| Incorrect battery model specified or approved | Responsible engineering and procurement parties |
| Battery not commissioned according to approved instructions | Responsible commissioning party |
| Confirmed transportation damage | Parties responsible under freight and sales contracts |
| Improper storage after delivery | Party responsible for storage and handling |
| Incorrect site test procedure | Party responsible for testing and approval |
| Charger incompatibility | Parties responsible for system design and integration |
| Unclear contractual acceptance criteria | Contracting parties and technical approval process |
This matrix is an investigation guide, not a legal determination of liability. For example, a manufacturer may have contractual obligations even where a separate subcontractor performed part of the work. Conversely, a distributor may assume responsibilities that differ from those of the original factory. The purchase contract, warranty terms, approved specifications, and applicable law determine the parties’ rights and obligations.
9. How Should an Overseas Distributor Handle the Customer Complaint?
For overseas distributors, this situation creates a challenge because they often act as the primary contact for the final customer. Even when the original batteries were manufactured by another company, the local importer may be expected to coordinate technical investigation and communicate the proposed resolution.
A useful first response should acknowledge the reported test result and request the evidence needed for analysis. The distributor should avoid making unsupported statements that either confirm or deny a manufacturing defect before the investigation is complete.
Information to Request from the Customer
The customer should provide the installation date, battery model, cell quantity, charger configuration, commissioning records, and complete discharge test report. Photos showing battery arrangement and electrical connections can also be valuable. If the battery supports essential power equipment, the distributor should ask whether the system remains operational and whether temporary backup arrangements are required. This information helps determine the urgency and technical scope of the problem.
10. Should the Battery Be Retested?
A retest may be justified if the initial test was conducted under incorrect or incomplete conditions. For example, the battery may not have received the required commissioning charge, or the discharge tester may have been configured incorrectly. However, retesting should not be used simply to disregard an unfavorable result.
Before repeating the test, the parties should document the identified problem, approved corrective actions, and new test procedure. The battery must be appropriately prepared, and the test should follow agreed acceptance criteria. For critical installations, the test plan must address the temporary reduction in available backup capacity. Repeated discharge tests can also place unnecessary stress on the battery and disrupt site operations.
11. What Corrective Actions May Be Appropriate?
The solution depends on the confirmed cause. If the battery was incompletely charged, the appropriate charging procedure and a valid retest may resolve the discrepancy. If excessive connection resistance caused premature voltage loss, correcting the installation may be necessary. If the battery model was incorrectly selected, the parties may need to reassess the design and consider a technically suitable replacement.
Where testing confirms that cells fail the agreed product requirements, replacement or other remedies may be appropriate under the purchase contract and warranty. In some disputes, commercial compensation may be negotiated. However, financial compensation should not be treated as a substitute for restoring the reliability of a safety-critical DC power system. Any battery remaining in service must still satisfy the applicable operational and safety requirements.
12. How to Prevent FAT and SAT Disputes Before Shipment
The most effective way to reduce these disputes is to establish common technical expectations before production. The supplier, EPC contractor, distributor, and end user should agree on the battery model, required discharge performance, test conditions, acceptance criteria, and responsibilities. Where necessary, a project inspection and test plan should be approved before manufacturing begins.
Recommended Pre-Shipment Agreement
| Item | Required Agreement |
|---|---|
| Battery model and quantity | Approved technical specification |
| Factory test scope | Tests, samples and records |
| Site test scope | Procedures and measurement points |
| Charging preparation | Approved commissioning instructions |
| Temperature conditions | Required reference or correction method |
| Discharge current | Defined current or duty cycle |
| Final voltage | Approved endpoint criteria |
| Test equipment | Accuracy and calibration requirements |
| Retesting | Conditions and responsible parties |
| Warranty claims | Evidence, procedure and remedies |
Written agreements do not prevent every technical problem, but they reduce ambiguity when difficulties occur. For overseas projects, this can save time and help maintain relationships between the supplier, importer, and final customer.
Frequently Asked Questions
Can a NiCd battery pass FAT but fail SAT?
Yes. Factory and site conditions may differ, and the installed system introduces additional factors such as cables, charger settings, installation quality, and storage history.
Does a passed factory test prove that the manufacturer has no responsibility?
No. Responsibility depends on the contract and verified cause. A factory test is important evidence, but it does not automatically resolve every later quality or compliance issue.
Can incorrect commissioning cause a new NiCd battery to fail a capacity test?
Yes. An incomplete or incorrect initial charging procedure can affect subsequent discharge performance.
Should the importer immediately replace batteries that fail SAT?
Not necessarily. The root cause should be investigated first, unless safety or contractual requirements demand immediate action.
What is the most important document in a FAT/SAT dispute?
There is no single document that resolves every dispute. The approved technical specification, test procedures, complete test records, commissioning history, and contract are all important.
Can an independent laboratory help resolve the disagreement?
Potentially. Independent testing may be useful when the parties cannot agree on the cause, provided the test procedure and acceptance criteria are agreed in advance.
Conclusion
A successful factory acceptance test followed by an unsuccessful site acceptance test does not automatically prove either manufacturing failure or installation error. The correct approach is to compare test conditions, examine the battery’s transportation and commissioning history, inspect the installed system, and review the complete technical evidence.
For overseas industrial battery distributors and EPC contractors, a structured investigation helps prevent unnecessary replacement costs and unsupported warranty disputes. Clear technical specifications and agreed acceptance procedures are the foundation of a successful industrial NiCd battery supply project.
Industrial NiCd Battery Supply for International EPC Projects
WUXI HUIZHONG POWER CO., LTD. supplies industrial nickel-cadmium batteries for substations, power plants, railway signaling, telecommunications, and other critical DC backup applications.
For project quotations, visit www.huizhongpower.com and provide your technical specifications, required battery models, quantity, destination country, and acceptance testing requirements.
Our team can discuss available products, technical documents, and project-specific supply requirements.